* Simply fill out the form below as best you can. And don’t sweat the details. * Your information will be kept strictly confidential. * Share your needs with us, We’ll contact you in very short time.
Planning a Custom Bag Order?
Send your bag type, quantity and target delivery date. We will review the specification and confirm the next step.
Who this guide is for: sourcing managers, DTC founders, activewear brand product managers, Amazon FBA sellers and gym-chain merchandise buyers who wrote “waterproof” on a brief and got four different quotes back, each describing a different bag.
The word “waterproof” carries no fixed meaning on a bag quote. One factory reads it as a spray finish on a woven shell. The second reads it as a PU coating on the reverse of 600D polyester. The third adds seam tape and a coated zip. The fourth quotes a welded body with a roll-top and comes back at twice the price of the first. All four answer the same brief honestly, and only one of them makes a bag that keeps a wet swimsuit off dry clothes on a train. Choosing waterproof material for bags starts with deciding which of those four bags you are actually buying.
The gap costs money in both directions. A brand that specifies a welded TPU body for a gym tote pays for performance the customer never uses and ships a bag that feels rubbery on the shoulder. A brand that specifies a coated woven shell for a kayak duffel gets returns after the first weekend, because the fabric held and the base seam did not. Between those two errors sit most of the waterproofing disputes that land in a sample room.
This guide separates the four construction levels, sets the materials side by side by weight, cold behaviour, print and weld compatibility, explains why seams and hardware leak long before the fabric does, describes how high-frequency welding works and which materials accept it, and shows how to write the level into a tech pack so that three factories quote the same bag. Test methods themselves, including how a hydrostatic head figure is produced, are covered in the companion guide on bag fabric testing and water column ratings; everything here is about materials, construction and specification.
Waterproof vs Water-Resistant Bag: Why “Waterproof” Is Not One Specification
A fabric can be rated. A bag cannot inherit that rating. The rating describes a flat piece of cloth with no needle holes, no zipper, no rivet and no closure, held under a rising column of water in a lab. Sew that cloth into a bag and you add several hundred holes along the base, a closure that opens, and four to eight metal penetrations for handles and rings. The bag performs at the level of its weakest opening, and that is almost never the fabric.
That is why a useful specification names a construction level rather than an adjective. Four levels cover nearly everything sold in this category.
The four things a factory might mean
A water-repellent finish. A chemical treatment on the face of a woven fabric that makes droplets bead and run off. It changes the surface, not the cloth. Rub it, wash it, or leave the bag in steady rain and the fabric wets out and passes water through. Repellent finishes are cheap, add no weight, and change nothing about the seams.
A coated fabric. A polyurethane or vinyl layer applied to the reverse of the woven cloth, which blocks water through the fabric field. This is what most quotes mean by waterproof material for bags. The cloth now holds back real pressure, so the water finds the stitch line instead.
A sealed-seam bag. The same coated cloth, with the inside of each seam covered by a heat-applied tape, or with critical seams welded where the coating allows. Water no longer walks through the needle holes. The zipper becomes the leak.
A welded, sealed system. A body made from a weldable sheet material, joined by fused seams instead of stitches, closed by a roll-top or a welded closure. No needle holes below the closure line, no zipper teeth, no rivets through the wall. This is the only construction that survives being dropped in a lake and pulled out again.
The plain-language ladder
Buyers get further with a behaviour description than with a number. Four sentences describe the ladder well enough to align a brand team, a factory and a customer-service script:
Splash-resistant. Handles a splash from a bottle or a two-minute shower between the car and the door. Contents damp if the rain continues.
Rain-resistant. Handles ten to twenty minutes of steady rain and a wet bench under the base. Contents dry. Contents wet if the bag sits out in rain for an hour or gets set in a puddle.
Weatherproof. Handles an hour or more of rain, a wet lawn and a soaked bike rack, because the seams are sealed and the closure has a flap or a coated zip. Not immune to a dunking.
Submersible. The closed bag can go under water and come back with dry contents, because the body is welded and the closure seals against itself.
The commercial rule that follows: call a bag water-resistant unless the body is welded and the closure seals, and describe submersion behaviour in the product copy rather than reaching for a rating scheme. A dry bag with a welded body and a three-fold roll-top is submersible. A duffel from the gym and training range in PU-coated 600D with stitched seams is rain-resistant, whatever number the fabric mill printed on its sheet.
The Four Construction Levels of Waterproof Material for Bags Compared
The table below is the one to hand a factory. Each row is a complete construction, not a fabric, and the water column figures describe the fabric used at that level rather than the finished bag. Where water gets in first is the column buyers skip and then discover on the return report.
Level
Construction
Typical fabric water column
Where water gets in first
Typical bag types
Relative cost
1 · Splash-resistant
DWR-finished woven polyester or nylon, uncoated or lightly finished, sewn seams
Roughly 100–400 mm
Through the fabric itself once the finish wets out, usually within minutes of steady rain
The four bag construction levels against typical water column range (mm, log scale)
Ranges describe the fabric used at each level and are industry-typical specification bands, not measurements of one roll. The finished bag performs at the level of its seams and closure, which sit below the fabric figure at levels 1 and 2.
Two things stand out on the chart. The step from level 1 to level 2 is the largest single jump in fabric performance a buyer can make, and it costs the least, because it is a coating decision on a fabric the factory already stocks. The step from level 3 to level 4 is smaller on the axis and much larger on the invoice, because it changes the material, the machinery and the pattern all at once.
The middle two levels are where most sourcing errors live. A level 2 bag with a good-looking coating figure gets sold as waterproof, and the first complaint arrives from a customer who set the bag on a wet pavement. A level 3 bag gets specified with taped seams and then fitted with a standard coil zip, which quietly returns the bag to level 2 performance in the one place water reaches first.
Waterproof Bag Materials Compared: Coated Polyester, Nylon, PVC Tarpaulin, TPU Film, PEVA and Laminated RPET
Once the level is fixed, the material decision follows from four questions: how heavy the bag is allowed to be, whether it will be used in cold weather, how the logo will go on, and whether the seams need to weld. The table sets the six materials that cover almost all custom waterproof bags against those questions.
Material
Typical weight
Cold-crack behaviour
Print compatibility
Weld compatibility
Relative cost
210D–600D polyester, PU-coated
Roughly 120–280 GSM
Stable well below freezing; heavy folding in cold can craze a thick coating over years
TPU film 0.15–0.5 mm, standalone or laminated to nylon or polyester
Roughly 150–500 GSM
Stays flexible far below freezing; no plasticiser to migrate
Heat transfer, pad print, screen with matched ink, welded patch
Yes, high-frequency and hot air
High
PEVA 0.10–0.25 mm
Roughly 90–200 GSM
Stiffens in cold and goes brittle at low temperature
Limited; screen print only, with modest wash durability
Yes, but welds are weaker than TPU or PVC
Lowest
Laminated RPET (recycled polyester with PU or TPU laminate)
Roughly 200–320 GSM
As polyester; the laminate sets the cold behaviour
Good; the same methods as virgin polyester
Only where the laminate is TPU
Moderate
Coated woven polyester and nylon
These two carry levels 1 to 3 and most of the volume in this category. Polyester is cheaper, holds colour better in sun, absorbs less water, and takes sublimation, which makes it the default for printed swim duffel bags and gym bags. Nylon is lighter at equal denier and drapes better, which earns it a place on packable and lightweight bags where every 20 g is argued over. Neither welds, because a thin PU coating gives the die nothing to fuse. Both accept seam tape.
The practical range is 210D for linings and light pouches, 420D for lightweight packs, 600D for the mainstream shell, and 840D nylon or 900D polyester for bases that meet wet ground. The guide to 600D polyester, GSM and coatings sets out how each coating pass changes the weight and the hand of that mainstream shell.
PVC tarpaulin
A polyester scrim with vinyl laminated on both faces, sold by finished weight rather than denier. It is the traditional dry-bag and gear-bag material, it welds faster and more forgivingly than anything else, and it wipes clean. The two objections buyers raise are weight and hand feel. At 500 GSM a 30 L roll-top runs heavier than the same bag in film, and the surface has a vinyl smell out of the carton that fades over a week or two. Cold performance depends on the compound: better grades stay workable at low temperature, cheaper grades stiffen and can crack at a hard fold. If the programme ships to cold markets, ask for the cold-fold behaviour of the specific roll rather than accepting “PVC tarpaulin” as an answer.
TPU film
Thermoplastic polyurethane is the material buyers usually mean when they want a technical-looking waterproof bag. It is supplied as standalone film from about 0.15 mm for light pouches up to 0.5 mm for structured dry bags, or laminated to a light nylon or polyester face for a fabric look with film performance. TPU holds its flexibility in cold, contains no plasticiser to migrate into printed graphics, welds cleanly, and can be supplied clear, translucent or pigmented. It costs more than PVC by a clear margin, and that gap is the single biggest driver of the price difference between two visually similar roll-top bags.
PEVA and laminated RPET
PEVA film is the low-cost option for wet pouches, toiletry bags and liners. It welds, it is inexpensive, and it will not carry structural load or survive rough handling. Reserve it for linings and pouches inside a stronger shell.
Laminated RPET brings recycled content to a waterproof programme. The recycled polyester base behaves like virgin polyester, and the laminate decides everything else: a PU laminate gives a level 2 or 3 fabric, a TPU laminate gives a weldable one. Stock colour depth is narrower than virgin, so a brand colour is more likely to need a lab dip. Venlinker describes recycled content by fibre and source on the tech pack and swatch tag, and leaves any documentation of that content to testing the buyer commissions from a lab of choice. The custom materials and colours page lists what is held in stock by weight and finish, and the bag material guide covers the woven fabrics in more depth.
Why Seams, Zippers and Hardware Leak Before the Fabric Does
Every waterproofing failure a factory sees in returns arrives through a hole somebody made on purpose. The fabric is rarely the culprit.
A lockstitch at 8 to 10 stitches per inch puts a needle hole every 2.5 to 3.2 mm along every seam. A 40 L duffel carries roughly 4 to 6 metres of seam, which is somewhere between 1,300 and 2,400 holes. A coated fabric rated at 3,000 mm has no bearing on any of them, because water passes a needle hole at effectively zero pressure. Gravity carries beaded water down the panel to the lowest seam, and the base seam is where it enters.
Three responses exist. Tape the seam on the inside with a heat-applied film, which needs a compatible coating to bond to and adds a step to the line. Weld the seam, which needs a weldable material. Or move the seam above the waterline, binding and turning the base so that the stitch line sits 30 to 50 mm up the side panel instead of at the point of contact. The third costs nothing and solves the most common complaint on a level 2 bag, which is a wet patch on the base after the bag sat on a wet floor.
The zipper, which is the weakest point on most bags
A standard coil or tooth zipper is a channel with a gap running its full length. Nothing about it resists water. The options above it, in order:
A coil zip under a storm flap. The flap does the work; the zip does none. Cheap, effective against rain falling from above, useless against submersion or a bag lying on its side in a puddle.
A coated coil zip. The tape carries a film laminate and the coil is set behind it, so the closed chain presents a continuous face. It slows water and resists rain running down a panel. It is not a seal, it stiffens with age and dirt, it needs a heavier slider pull, and it costs several times a standard zip.
A welded zip in a welded tape. The zip tape itself is welded into the body panel rather than stitched, which removes the needle holes along both sides of the chain. This is the only zipper construction that belongs on a level 4 bag, and it still ranks below a roll-top for pressure.
A roll-top. No mechanism at all. The top hem carries a stiffener strip, the user folds the opening down three or more times, and a side-release buckle holds the roll closed. Each fold multiplies the path length water must travel. Three folds is the working minimum for a bag described as submersible; two folds is a rain closure.
Roll-top geometry deserves a line on the tech pack. The panel above the fill line must be long enough for the folds, which usually means 120 to 180 mm of extra height, and the buckle webbing must be positioned so the roll closes flat rather than pleating at the ends. A bag that rolls into a wedge leaks at the corners no matter how many folds the user makes. Which coil gauge, slider and side-release buckle to name alongside that geometry is covered in the guide to zippers, buckles and webbing.
Hardware penetrations
Every rivet, grommet, foot stud and stitched D-ring anchor is a hole through the wall. On a level 4 bag the rule is simple: nothing penetrates the body below the closure line. Handles, D-rings and compression anchors are carried on welded patches that bond to the outside face and transfer load through the weld area rather than through a fastener. On a level 3 bag, penetrations are allowed but should be sealed and kept high: base feet are the classic failure, because they sit at the exact point where the bag meets standing water.
Drain grommets are a deliberate exception. A shower caddy or a mesh-panelled wet-gear bag is designed to let water out, and fitting it with a sealed base defeats the product. Decide early whether the bag is meant to hold water in, keep water out, or let water through, because those three intentions produce three different patterns.
Closure or fitting
Realistic performance
Cost impact
Where it belongs
Standard coil zip, no flap
No water resistance at the chain
None
Interior pockets, dry-side compartments
Coil zip under a storm flap
Handles rain from above; fails on a wet surface
Low
Level 2 duffels and backpacks
Coated coil zip
Resists running rain; not a seal; stiffer action
Moderate to high
Level 3 commuter and travel bags
Welded zip in welded tape
Holds under splash and brief immersion
High
Level 4 pouches and gear bags
Roll-top, 3+ folds with buckle
Holds under full submersion when rolled correctly
Low on a welded body
Level 4 dry bags and duffels
Hook-and-loop welded flap
Splash and rain; simple, no hardware
Low
Wet pockets, liners, kids’ bags
Riveted D-ring or foot stud
A hole through the wall
Low
Level 1 to 3 only, above the waterline
Welded patch anchor
No penetration; load spread over the weld
Moderate
Level 4 bodies
Hardware choice interacts with the material more than buyers expect, and the custom trims and hardware page covers which buckles, sliders and rings the sample room stocks against each construction.
High-Frequency Welding Explained: Which Bag Materials Weld and Which Do Not
High-frequency welding, also called radio-frequency or dielectric welding, is how a level 4 bag body gets built. Venlinker runs it in-house, so this section describes what actually happens on the machine rather than what the brochures say.
What high-frequency welding is
Two plies of material are laid between a shaped brass die and a flat bed. The machine applies pressure and then sends a high-frequency electric field, typically in the 27 MHz region, through the stack. The field makes the polar molecules in the material oscillate. Internal friction turns that motion into heat, and the heat is generated inside the material rather than conducted in from a hot surface. The two plies soften, merge across the interface, and then cool under continued pressure until the joint sets. The result is one piece of material where there were two, not two pieces held together by an adhesive or a thread.
The cycle is short, usually a few seconds, and it is controlled by three settings: power, weld time and cooling time under pressure. A weld with too little cooling time looks fine on the machine and delaminates in the carton, because the operator lifted the die before the joint had set.
Which materials weld and which do not
The material has to be polar. That is a property of the polymer, and it is not negotiable by turning the power up.
Welds well: PVC, TPU, PEVA, and woven fabrics laminated with a sufficient thickness of any of the three.
Welds poorly or not at all: polypropylene and polyethylene, silicone-finished fabric, and plain polyester or nylon carrying only a thin PU coating. There is no melt layer for the die to fuse, and pushing power at these materials scorches the face without making a joint.
The grey zone: heavily PU-coated fabric and thin laminates. Some accept a weld that holds for handling but not for load. A sample-room weld trial on the exact roll settles it, and that trial belongs before the tech pack is signed, not after.
This is the reason a factory quoting a “welded” bag in PU-coated 600D polyester should be asked to demonstrate it. The honest version of that construction is stitched-and-taped, which is level 3, and it is a good bag; it is not a welded one.
Weld width and how to check a weld
Weld width comes from the die and belongs on the drawing:
Body and side seams: typically 8 to 12 mm on TPU or PVC. Narrower welds concentrate stress on a thin line and peel.
Patch anchors for handles and D-rings: typically 10 to 20 mm of bonded area around the fitting, sized to the load rather than the look.
Roll-top hems and stiffener channels: typically 10 to 15 mm, with the stiffener fully enclosed so it cannot migrate.
Decorative or logo patches: 3 to 5 mm is enough, since they carry no load.
Two checks separate a good weld from a passable one. The first is destructive: cut a strip across the weld and pull it. A correct weld tears the parent material beside the joint and leaves the joint intact. A weld that peels apart cleanly along the interface was under-powered or under-cooled. The second is the fill-and-hold check on finished bags. The bag is closed, filled with air or water, and held while the operator looks along every seam and every patch for beads or bubbles. Air is faster on a line and catches pinholes; water catches slow seepage and is the better check on a first-off unit.
Custom dies are tooling, and a new body shape or a new patch profile carries a die-making step. Buyers planning an original welded silhouette rather than an adapted stock pattern should budget lead time for that step and discuss it early through custom design and structure, since a shape that welds in two passes costs materially less than one that needs five.
How to Specify Waterproofing in a Bag Tech Pack
The instruction that fixes almost every waterproofing dispute is short: state the level, not the word. A tech pack that says “waterproof” invites four different bags. A tech pack that carries five lines gets four comparable quotes.
The five lines are fabric, coating or film, seam treatment, closure, and how the result will be checked. Each one is a decision somebody makes; if the buyer does not make it, the factory does.
Tech pack line
What to write
What happens if you leave it blank
Shell fabric
Fibre, denier or film thickness, weave, face finish, colour reference
The factory picks the cheapest roll that matches the colour
Coating or film
PU single or double pass, PVC weight, TPU thickness, which face it sits on
A single light PU pass, quoted as waterproof
Seam treatment
Stitched / stitched and taped / welded, with weld width and which seams
Stitched throughout, including the base
Closure
Zip type, flap, roll-top with minimum fold count and roll height
A standard coil zip
Hardware and penetrations
Which fittings may penetrate the wall, and the minimum height above the base
Riveted feet and D-rings wherever the pattern is easiest
Check method
Fill-and-hold on first-off, on a sample per lot, or on 100% of units, with hold time
A visual check only
A worked spec line for a level 4 bag
Body: 0.30 mm TPU film laminated to 210D nylon, matte face, colour to approved lab dip.
Seams: high-frequency welded, 10 mm weld width on body and base seams, no stitching anywhere below the roll line.
Closure: roll-top, minimum three folds, 180 mm roll height above the fill line, 25 mm welded stiffener bar in the top hem, 25 mm side-release buckle.
Hardware: two D-rings on welded patches, 15 mm bonded margin, positioned on the upper third of the side panels. No rivets, grommets or foot studs in the body.
Logo: heat-transfer film on the front panel, 120 × 40 mm, applied before body assembly.
Check: every unit filled to roughly 60% with air, closed at three folds, submerged and held 60 seconds at inline inspection; any bead or bubble rejects the unit.
A worked spec line for a level 3 bag
Shell: 600D polyester, plain weave, water-repellent face finish, double-pass PU on the reverse, 240–280 GSM.
Seams: stitched at 8–10 stitches per inch, heat-applied tape on all base and lower side seams to 150 mm above the base; upper seams stitched only.
Base: bound and turned so that the stitch line sits 40 mm above the contact face.
Closure: coated coil zip on the main opening, under a 35 mm storm flap; standard coil zips on interior pockets.
Hardware: riveted feet permitted, minimum 20 mm above the base contact face, sealed washers.
Check: spray check on first-off; taped seams inspected on 100% of units at final inspection.
Both examples name a number on every line, which is what makes them quotable. The bag tech pack guide shows where these lines sit alongside the rest of a bag BOM, and the RFQ checklist turns them into questions three suppliers can answer in the same format. Buyers who want a specification written this way before sampling can send the brief through the get a quote form and get the waterproofing section filled in as part of the reply.
Matching the Waterproofing Level to the Use Case
The right level is the lowest one that solves the actual problem. Over-specifying is not a safe default; it adds weight, stiffness and cost the customer notices immediately, while the failure it protects against may never occur.
Use case
Level
Typical construction
Product types
Wet swimsuits and pool gear
4 inside 2
PU-coated woven shell, welded TPU or PEVA wet compartment, hook-and-loop or coated zip on the wet side
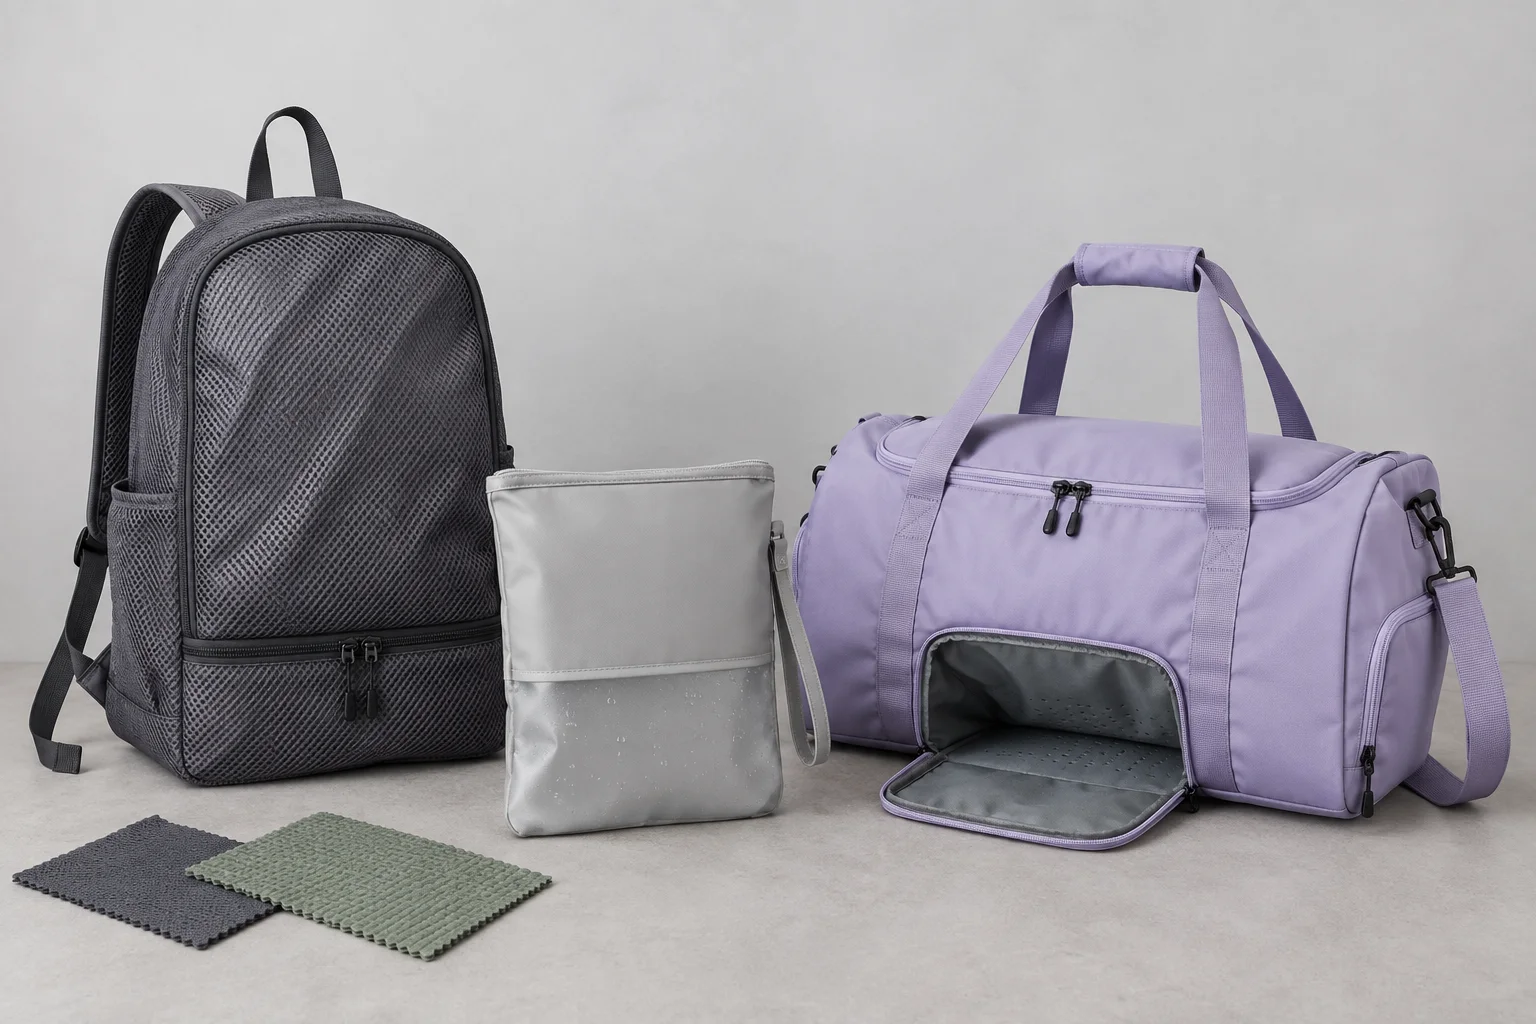
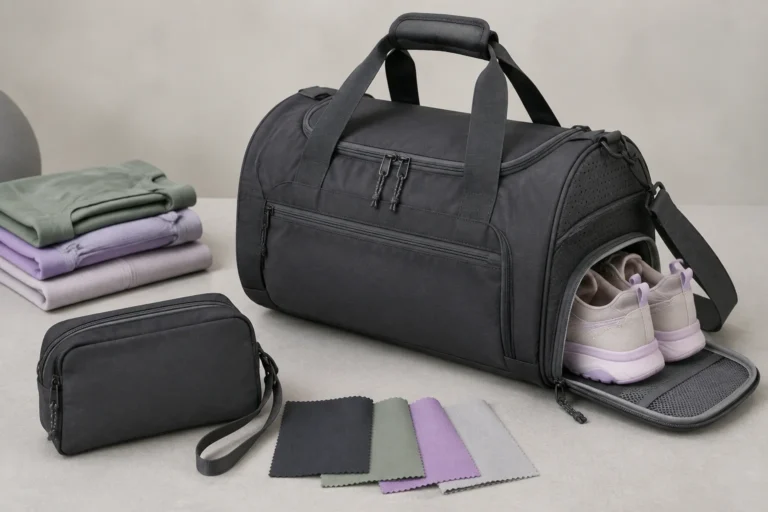
The pattern that works for swim and gym is a welded compartment inside a conventional bag. The customer needs one part of the bag to hold water away from everything else, and the rest of the bag needs to be light, printable and cheap to make. Building the whole shell at level 4 solves the wrong problem and produces a bag nobody wants to carry to a class. Gym and studio chains ordering member bags and activewear brands adding a wet-gear SKU almost always land on this construction after the first sample round. How that welded cell is sized and placed against the shoe compartment and the dry space is worked through in the guide to wet-dry gym bags and shoe compartments.
Outdoor and travel programmes
Open-water and paddle use is the one case where level 4 across the whole bag is right, because the failure mode is submersion rather than rain. Trail and travel sit at level 3: sealed base, coated zip, and a weight the customer will actually carry. Amazon FBA sellers should note that submersion claims in a listing invite testing by customers, so the listing copy and the construction level need to agree before the first shipment.
Commuting and everyday programmes
A rain-commute bag lives or dies on the zipper and the base. Get those two right and a coated woven shell handles the rest. Startup and DTC brands launching a first commuter pack often start at level 2 with a bound-and-turned base, then move to level 3 on the reorder once reviews show where water reached.
Questions to Ask a Waterproof Bag Manufacturer Before Sampling
These ten questions separate a supplier who is quoting a construction from one who is quoting a word. Ask them before the sample, and put the answers on the tech pack.
Which of the four levels are you quoting? A supplier who cannot place their own quote on the ladder is guessing.
What is the exact fabric or film, and what is its coating or thickness? Expect a fibre, a denier or a millimetre figure, a coating type and a pass count.
How are the body seams joined? Stitched, stitched and taped, or welded. If welded, on which machine and with what weld width.
Which seams are treated, and which are not? Partial tape coverage is a legitimate choice, and the buyer should know where it stops.
What closure, and what is its realistic performance? A coated zip is not a seal, and a supplier who says it is should be pressed.
On a roll-top, how many folds does the design assume and how much roll height is in the pattern? Three folds and 120 to 180 mm is the working answer.
What penetrates the body wall, and how high above the base? On a level 4 bag the answer should be nothing.
Do you weld in-house or subcontract it? Subcontracted welding adds days and puts the critical operation outside the factory’s own inspection.
How is each lot checked, and can I see the record? Ask for a fill-and-hold procedure with a hold time and a sample rate.
Can I commission an independent test on the finished bag? The factory should be able to stage units for a lab or inspection body the buyer names.
Answers that come back as “yes, waterproof, no problem” are the ones to worry about. A supplier who has built these bags will answer question 3 and question 7 in specifics without prompting. Buyers comparing three factories can score the answers side by side, or contact the sample room with a reference bag and ask which level it actually is.
How Venlinker Builds and Checks Custom Waterproof Bags
Venlinker is Your Trusted Custom Waterproof Bag Manufacturer in China, and the reason waterproofing sits close to the centre of what the factory does is that high-frequency TPU and PVC welding runs in-house on the same floor as the sewing lines, rather than at a subcontractor two hours away.
Welding and construction
The Huadu District factory in Guangzhou has run since 2010 across 5,000 m² with 10+ production lines and 500+ staff, producing 50,000+ bags a month. Welded work moves between the welding stations and the sewing lines inside one building, which matters for the bags most buyers in this category order: a stitched shell with a welded wet compartment, where the two operations have to meet on the same pattern. Weld width, die profile and cooling time are set at the sample stage and recorded against the golden sample, so a repeat order six months later runs the same joint. The manufacturing capabilities page covers what each line is set up for.
Materials
Fabric and film come through a network of 200+ verified fabric suppliers, and the material sourcing team records coating type, thickness, weight and weldability against each roll so that “TPU” on a tech pack maps to a specific film rather than a category. Where a programme needs a film outside the network, a specific PVC compound for cold markets or a particular RPET laminate, sourcing quotes the extra lead time up front instead of discovering it at cutting.
Samples with a fill-and-hold check
Samples run in 5–7 working days with one free revision, and a welded sample ships having been filled and held before it goes in the box. Where the buyer wants to see the joint rather than trust it, the sample room includes a cut weld strip so the buyer can pull it by hand. The sample development page sets out what the sample room needs to hit that window, and buyers can request a free sample to compare a welded TPU body against a taped-seam coated woven in hand before choosing a level.
Inspection
Welded lots get a fill-and-hold check at inline production inspection as well as at the end, because a pinhole found at inline costs one panel and a pinhole found at final costs a finished bag. Every order passes 100% pre-shipment inspection by the factory’s own team. Third-party inspections from SGS, BV or TUV are welcome on any order, commissioned and paid by the buyer, and lab testing on fabric or finished bags can be arranged the same way through third-party inspection support.
MOQ starts at 300 pcs per style per colourway, which lets a brand test one waterproof SKU alongside an existing range rather than committing a season to it. Private label programmes running several bags under one identity usually specify a shared film and colour across the welded pieces so the set reads as one family. Retail and FBA packing is handled through custom packaging and retail prep, and logo application on welded surfaces is set up under custom graphics and printing, where transfer film and welded patches usually beat screen print on a flexible film face. A buyer with a construction level already chosen can send it for a quote and get the weld width, closure and check method priced as separate lines rather than folded into one number.
Waterproof vs Water-Resistant Bag FAQ
What is the difference between a waterproof bag and a water-resistant bag?
A water-resistant bag slows water down. A waterproof bag stops it. In construction terms, water-resistant covers levels 1 to 3: a repellent finish, a coated fabric, or a coated fabric with sealed seams and a coated zip. Waterproof means a welded body with no needle holes below the closure line and a closure that seals against itself, usually a roll-top with three or more folds. A bag with a stitched base and a coil zip is water-resistant no matter what the fabric mill’s sheet says.
Is PU-coated 600D polyester waterproof?
No. PU-coated 600D polyester is rain-resistant, with a typical fabric water column in the 500–3,000 mm band depending on how many coating passes it carries. Water enters the finished bag through the needle holes along the base seam and through the zipper, both at effectively zero pressure. It is the right fabric for gym duffels, totes and backpacks, and the wrong one for anything that will be submerged.
Which is better for a waterproof bag, TPU or PVC?
They solve the same problem at different price and weight points. PVC tarpaulin is cheaper, welds most easily, wipes clean, and is heavier and stiffer in cold weather. TPU film is lighter for the same performance, stays flexible in cold, carries no plasticiser, welds cleanly, and costs noticeably more. Programmes selling on a technical positioning or shipping to cold markets usually choose TPU; programmes selling on price or building large gear bags usually choose PVC.
Can a bag with a zipper be waterproof?
Under splash and brief immersion, yes, if the zip tape is welded into the body rather than stitched to it and the closure is designed around the slider. Under sustained submersion, a zipper is still the weakest point on the bag. A roll-top with three or more folds outperforms any zipper closure, which is why dry bags and paddle-sport duffels use one. A coated coil zip, which some suppliers call waterproof, resists running rain and does not hold under pressure.
How many folds does a roll-top dry bag need?
Three is the working minimum for a bag described as submersible, and the pattern needs roughly 120 to 180 mm of roll height above the fill line to allow them. Two folds gives a rain closure. The roll also has to close flat: if the top hem pleats at the ends instead of folding cleanly, water finds the corners regardless of the fold count, which is why the stiffener bar and the buckle position belong on the drawing.
Can I print a logo on a welded TPU or PVC bag?
Yes. Heat-transfer film is the usual method on a flexible film face because it moves with the material, and welded patches in a contrasting film give a durable raised logo with no ink at all. Screen print works with a matched ink system. Embroidery does not belong on a welded body, since the needle holes defeat the construction. The logo method guide compares the methods by durability and minimum size, and custom logo and branding lists what the sample room needs in the artwork file.
What is the MOQ and lead time on a custom welded waterproof bag?
MOQ starts at 300 pcs per style per colourway. Samples take 5–7 working days with one free revision, and a welded sample includes a fill-and-hold check before it ships. Bulk production runs roughly 25–35 days at 300–1,000 pcs and 30–40 days at 1,000–5,000 pcs, with repeat orders at 20–30 days. An original welded silhouette that needs a new die adds tooling time at the front of that schedule; adapting a stock body shape does not. The MOQ guide sets out how the tiers work across a mixed order.
Summary: How to Specify Waterproof Material for Bags
The word on the brief is the problem. Replace it with a level, a material and a seam treatment, and three factories will quote the same bag.
Name the construction level, not the adjective. Level 1 is a repellent finish, level 2 is a coated fabric with stitched seams, level 3 adds taped seams and a coated zip, level 4 is a welded body with a roll-top or welded closure. Only level 4 survives submersion, and only level 4 should be described as waterproof in retail copy.
Match the material to the level and the climate. PU-coated 210D–840D polyester and nylon carry levels 1 to 3 and do not weld. PVC tarpaulin, TPU film from 0.15 to 0.5 mm, PEVA and TPU-laminated RPET weld, and the choice between them turns on weight, cold behaviour and cost. Ask about cold-fold behaviour before shipping a PVC bag to a cold market.
Specify the seams, the closure and the check. Needle holes at 8–10 stitches per inch leak at zero pressure, zippers leak next, and rivets below the waterline leak after that. Write weld width, roll-top fold count and roll height, allowed penetrations and a fill-and-hold procedure with a hold time into the tech pack.
Brands ready to move from a level to a sampled bag can send the specification through the get a quote form, or contact Venlinker to have the waterproofing section written before the rest of the tech pack is finished. A first run at 300 pcs can follow the OEM/ODM workflow from swatch and weld trial to golden sample to bulk, with the same construction level carried through every step. Distributors and retailers stocking a waterproof range across price points can see how the levels ladder in the swim and wet gear range, and buyers comparing suppliers on this topic will find the questions above already built into the supplier comparison guide.
Need a Waterproof Bag Built to a Level, Not a Word?
Venlinker builds custom dry bags, welded wet compartments, swim duffels and rain-ready commuter packs for activewear brands, DTC founders and Amazon FBA sellers, with in-house high-frequency TPU and PVC welding, film and fabric from 200+ verified suppliers, samples in 5–7 working days with a fill-and-hold check, 100% pre-shipment inspection and MOQ from 300 pcs per style.