* Simply fill out the form below as best you can. And don’t sweat the details. * Your information will be kept strictly confidential. * Share your needs with us, We’ll contact you in very short time.
Planning a Custom Bag Order?
Send your bag type, quantity and target delivery date. We will review the specification and confirm the next step.
Bag Hardware Guide: Zipper Gauges, Buckles, Webbing and Sliders Explained
Bag zipper sizes explained for sourcing teams: #3, #5, #8 and #10 gauges, coil vs Vislon vs metal, buckles, webbing widths and a worked hardware BOM block.
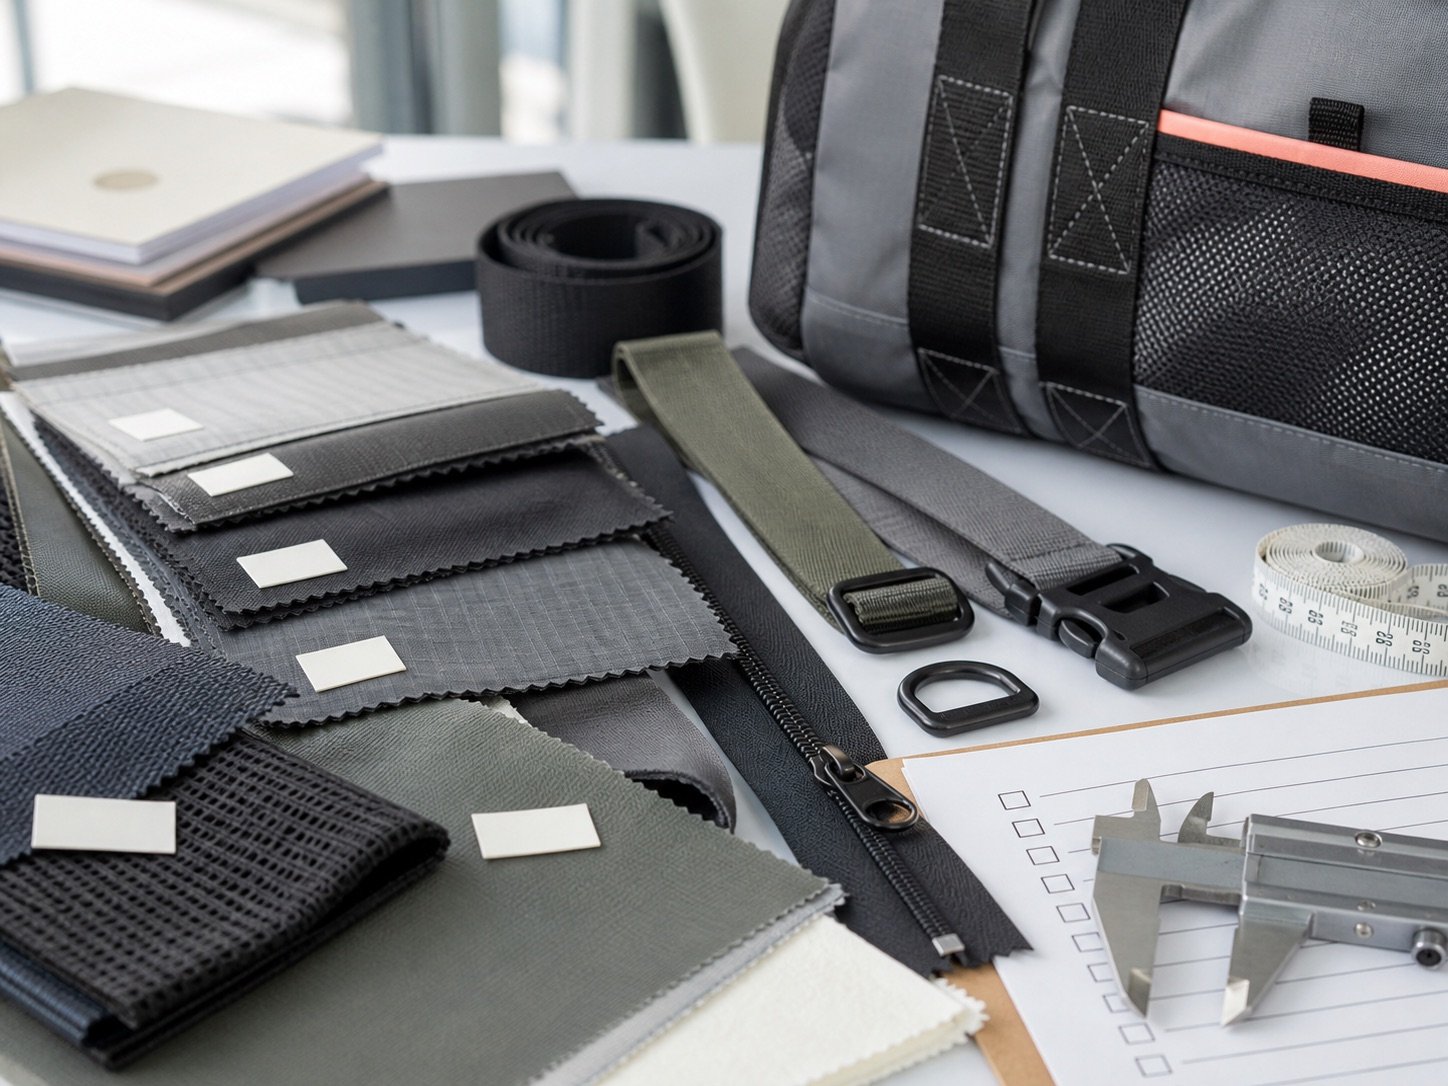
Sports bag materials zipper webbing stitching and quality inspection details
Who this guide is for: sourcing managers, DTC founders, activewear brand product managers, Amazon FBA sellers and gym-chain merchandise buyers who are holding a quote where the hardware line reads “metal zipper, plastic buckle” and need to know which figures to pin down before the first sample is cut.
Bag zipper sizes are the single most useful thing a buyer can pin down on a quote, and the line item that quotes most often leave vague. A gauge number, a chain type, a slider style and a webbing width take about ninety seconds to write and they decide whether a duffel survives two years of gym use or comes back through customer service in month five. Fabric gets the attention because it is 35–50% of unit cost. Hardware is usually somewhere in the region of 5–12% of the same cost, and it accounts for the majority of what buyers describe as a warranty claim.
That gap is the reason this guide exists. A brand can spend two weeks arguing about 600D against 900D and then accept “plastic buckle, standard zipper” on the same sheet, which hands the factory a free choice between hardware that costs a few cents more and hardware that costs a few cents less. The factory will usually choose to the price it was asked to hit. Specifying hardware precisely is the cheapest quality improvement available on a sports bag, because the cost delta between the weakest acceptable component and a properly matched one is small enough to disappear inside normal quote variance.
This guide covers zipper anatomy in plain terms, the #3, #5, #8 and #10 gauges with the chain widths and pull-strength bands that separate them, coil against Vislon against metal, sliders and pullers, buckles and adjusters, webbing widths in polyester, nylon and cotton, metal finishes and what chlorine and sweat do to them, custom moulded hardware as a branding surface, and a worked hardware schedule you can paste into a tech pack before you request a quote.
Bag Hardware Failure: Why Zippers and Buckles Break Before the Fabric Does
Ask any factory quality team which component generates returns and the answer is consistent across bag categories. Shell fabric rarely fails inside a normal product life. A 600D PU-backed polyester panel will scuff and fade long before it tears, and the denier and coating fundamentals behind that behaviour are well understood. Hardware fails differently: it fails suddenly, it fails at a single point, and the bag becomes unusable the moment it does.
The three failure modes buyers actually see
A slider spreads. The two flanges inside the slider body open under repeated load until the chain no longer closes behind it. The zipper looks fine and simply stops zipping. This is the most common single complaint on an overstuffed duffel, and it is almost always a gauge problem rather than a brand problem: a #5 slider was asked to do a #8 job.
A puller detaches. The tab separates from the slider, usually because a moulded pull was attached through a thin bail or a cord pull was knotted rather than crimped. The zipper still works with a fingernail, which is enough for a customer to review the bag as cheap.
A strap anchor pulls out. Webbing tears away from the shell, or the stitching that holds it does. On a 20 kg equipment load the failure point is usually the bar-tack, not the webbing itself. Bar-tacking at every anchor is a construction decision that costs seconds of machine time and prevents a return that costs a whole unit.
Why the cost argument favours the buyer
Hardware sits in a narrow cost band. Stepping a main compartment from a #5 coil to a #8 coil on a 40 L duffel adds a small single-digit percentage to unit cost. Stepping from an unbranded slider to a branded one at the same gauge is a similar order of change. Adding a second slider so the zip opens from either end is cheaper again. Set that against a return rate: on a 3,000-piece run, a hardware upgrade that costs a fraction of a percent of the order value pays for itself if it prevents a handful of replacements plus the freight to send them.
The practical conclusion is that hardware should be over-specified relative to the fabric, not matched to it. A 600D bag with #8 zips and 38 mm webbing outlives a 900D bag with #5 zips and 25 mm webbing, because the fabric on the second bag will still be intact when the zipper stops closing. Buyers building a spec around this trade-off will find the wider picture in the cost factors guide.
Zipper Anatomy Explained: Tape, Chain, Element, Slider, Puller and Stops
Most hardware disputes come from vocabulary. A buyer writes “zipper”, a factory reads “zipper”, and the two parties are picturing different objects. Six parts make up every zipper on a bag, and naming them individually is what makes a specification enforceable.
Tape is the woven fabric strip the elements sit on. Bag zippers use polyester tape, typically 25–35 mm total width for a #5 and 30–40 mm for a #8. The tape is what gets sewn, so tape width belongs on a tech pack alongside the gauge: a narrow tape gives the sewing operator less to grip and moves the stitch line closer to the chain.
Chain is the two rows of elements once they are engaged. Chain width, measured across the closed chain, is the number that actually defines a gauge, and it is the figure to ask for when a supplier’s “#5” looks smaller than the last supplier’s “#5”.
Element (or tooth) is the individual part that interlocks. On a coil zipper the element is a continuous nylon monofilament wound into a spiral and stitched to the tape. On a moulded zipper each tooth is injected onto the tape separately. On a metal zipper each tooth is a formed and clamped piece of brass, aluminium or nickel-plated alloy.
Slider is the moving body that opens and closes the chain. Its internal geometry, wall thickness and material set the load the zipper can take. A slider is specified by gauge, lock type and finish.
Puller is the tab hanging from the slider. It is the most visible piece of hardware on the bag and the cheapest place to put a brand mark.
Stops limit slider travel. A top stop prevents the slider running off the top of the chain. A bottom stop does the same at the base of a closed-end zipper. On a separating zipper the bottom stop is replaced by a box on one tape and an insert pin on the other, which is the mechanism that lets the two halves come fully apart on a jacket-style opening or a fold-flat gear bag.
Closed-end, open-end and two-way
A closed-end zipper is joined at the bottom and is the default for pockets, main compartments and pouches. An open-end or separating zipper carries the box and pin and is used where a panel must lay flat, common on helmet and gear bags that open like a clamshell for equipment access. A two-way zipper runs two sliders on one chain, either head-to-head for a duffel that opens from either end, or head-to-tail so a rucksack lid can be vented from the bottom. Two-way head-to-head is standard on gym duffel bags and is worth specifying by name, because a single-slider duffel forces the user to walk the slider the full length of the bag every time.
Bag Zipper Sizes Explained: #3 vs #5 vs #8 vs #10
The gauge number is an approximate reference to the chain width in millimetres when the zipper is closed. A #5 chain is roughly 5–6 mm across, a #8 roughly 8–10 mm. The number is a family designation rather than an exact measurement, and it varies slightly by chain type and manufacturer, which is why a chain-width figure in millimetres is a better line on a tech pack than the gauge alone.
Pull-strength descriptors here are relative bands across the four gauges, not measured figures. A buyer who needs numbers for a retail specification should commission a lateral-pull or reciprocating-cycle test from a lab of their choice on the actual chain, and the same principle covers abrasion and colour transfer, which the bag fabric testing guide sets out in full.
Zipper chain width and relative pull-strength band by gauge
Left: typical closed-chain width in millimetres. Right: an indicative relative band, scaled so that #10 sits at the top of the range. Bands are comparative guidance across gauges, not test results; commission a lab test on the actual chain if you need figures for a retail specification.
Matching gauge to compartment, not to bag
The mistake that produces spread sliders is specifying one gauge for the whole bag. A duffel does not need #8 on the shoe tunnel and the interior valuables pocket; it needs #8 where the load concentrates and #3 or #5 everywhere else. Weight is the reason. A 60 L team duffel with #10 on every opening carries several hundred grams of chain, and the customer feels every gram of it before the bag is loaded.
A working default for a 35–45 L gym bag: #8 two-way head-to-head on the main opening, #5 on front and side pockets, #5 on the wet or shoe compartment, #3 on the interior zip pocket. Scale up one gauge on the main opening for anything above 55 L or anything carrying rigid equipment, and the sports equipment backpacks category is where that step usually happens. Scale down for drawstring gym bags and light pouches, where a #3 or #5 is the whole zipper budget.
Coil vs Vislon vs Metal Zipper Chain Types Compared
Gauge answers “how big”. Chain type answers “made of what”, and it changes weather behaviour, cold performance, repair behaviour and how the zipper looks under a logo.
Chain type
Element construction
Weather behaviour
Self-healing
Cold performance
Branding surface
Relative cost
Coil (nylon monofilament)
Continuous spiral stitched to tape
Good; sheds water, dries fast, no corrosion
Yes; a slider run back over a misaligned chain usually reseats it
Stays flexible in cold; no brittleness in normal use
Tape can be printed or dyed; elements dye with the tape
Lowest
Vislon / moulded plastic
Individual acetal or polyacetal teeth injected onto tape
Good; no corrosion, sheds water
No; a broken tooth is a dead zipper
Tough but stiffer than coil in deep cold
Teeth can be moulded in colour; strong visual statement
Low to moderate
Metal (brass)
Formed and clamped brass teeth
Tarnishes; reacts to salt and chlorine
No
Stiffest of the four in cold; conducts heat away from fingers
Plated finishes, engraved pullers
Moderate to high
Metal (aluminium)
Formed aluminium teeth
Lighter than brass; oxidises and can mark light fabric
No
Stiff in cold
Anodised colours available
Moderate
Metal (nickel-plated alloy)
Formed alloy teeth with plating
Plating protects until it wears; then the base corrodes
No
Stiff in cold
Bright, gunmetal or matte black plating
Moderate
Where each type belongs on a sports bag
Coil is the default across this category and the correct default. It is light, it survives a wash cycle, it does not corrode next to a wet swimsuit, and its self-healing behaviour means a customer who forces a chain out of alignment usually recovers it themselves rather than contacting the brand. Coil is what belongs on mesh swim bags, wet-dry gym bags, yoga bags and the overwhelming majority of duffels and backpacks.
Vislon buys visual weight. Chunky moulded teeth read as technical and outdoor, they can be moulded in a brand colour that contrasts against the shell, and at #8 and #10 they carry serious load. The trade is that a single sheared tooth ends the zipper’s life, and moulded chain does not sit as flat around a tight radius. It suits helmet and gear bags, equipment cases and any bag where the zipper is part of the design language.
Metal is a styling choice on sports bags rather than a performance one. Brass at #5 on a work-gym backpack front pocket reads as considered and adds a weight the customer notices in the hand as substance. Metal on anything that meets chlorine, salt or persistent sweat is a service problem waiting to arrive, covered in more detail in the finishes section below.
Water-resistant and reverse-coil zippers
A reverse-coil zipper turns the chain over so the coil sits on the inside of the bag and the flat back of the tape faces out. It looks cleaner, it stops the coil catching on the contents, and it is the base construction for water-resistant zips.
A water-resistant zipper is a reverse coil with a polyurethane or TPU film laminated over the tape face. The film sheds spray and light rain along the zip line, which is where an unsealed zipper leaks first. It is water-resistant, not waterproof: water finds the slider gap, the stops and the needle holes. Anything sold as genuinely waterproof needs welded seams and a roll-top or a properly sealed closure, and the distinction between waterproof and water-resistant construction is worth settling before a zipper is specified at all. Water-resistant zips also run stiffer than plain coil, need a stronger pull, and cost more, so they belong on the openings that face weather rather than on every pocket.
YKK vs SBS Zipper and Unbranded Chain: What Actually Differs
Buyers ask about brand more than any other hardware question, usually framed as YKK against SBS. The honest answer is that the difference lives in consistency, availability and documentation rather than in a single quality verdict.
YKK is the reference point most tech packs are written against. Specifying it gives a buyer a chain with a stable dimensional standard across factories and years, a slider that will match a replacement ordered two seasons later, and a marked slider that retail buyers and marketplace listings recognise. It carries the highest cost tier of the three and, on less common gauges, colours or finishes, the longest lead time, because a specific chain colour in a specific gauge may need to be ordered rather than drawn from stock.
SBS and comparable branded chains sit a tier below on cost and are widely stocked in China in the gauges and colours a sports-bag line uses daily. Consistency within a colour and gauge is good, lead times are short, and for a bag that will never carry a repair programme this is where a large share of the category’s volume actually sits.
Unbranded chain covers a wide spread. Some of it is made in the same industrial cluster to the same dimensions and performs indistinguishably in normal use. Some of it varies roll to roll in slider wall thickness or plating quality in ways that only show after a few hundred cycles. The risk is not that unbranded chain is bad; it is that “unbranded” describes a category rather than a specification, so the buyer cannot tell which roll they received.
How to handle brand on a quote
Buyer-nominated hardware is normal practice and no supplier should treat it as unusual. A brand that names YKK on the tech pack gets YKK, with the cost and lead-time implications visible on the quote line rather than absorbed silently. Venlinker sources to nomination through the material sourcing team and will quote the nominated item and an equivalent side by side so a buyer can see what the nomination costs before committing.
Where a buyer has no brand preference, the useful instruction is not “any zipper” but a specification the factory can be held to: gauge, chain type, tape width, slider lock type, finish, and a requirement that the same supplier and article number be used across the whole order and any reorder. That last clause matters more than the logo on the slider. A bag that ships with three different sliders across three cartons looks like a quality failure even when every slider works.
Zipper Sliders and Pullers: Auto-Lock, Double Sliders and Custom Pull Tabs
The slider is the part that fails and the puller is the part that gets seen. Both deserve their own line on a tech pack.
Lock types
An auto-lock slider has a small pin that drops into the chain whenever the puller lies flat, holding the slider in place until the puller is lifted. It is the right default for main compartments on duffels and backpacks, because it stops a loaded bag creeping open under its own weight.
A non-lock slider runs freely in both directions. It is faster to use, quieter, and correct on light pockets and on anything a user opens one-handed while moving, such as a running belt or a hydration pack pocket.
A pin-lock or semi-auto slider locks only when the puller is pushed into a specific position. It appears on bags where a deliberate hold is wanted without the friction of a full auto-lock.
A double slider puts two sliders on one chain. Head-to-head is the duffel standard and lets the user open the bag from whichever end they are standing at. Head-to-tail lets a compartment be vented or accessed from the bottom without opening the top, which is how a convertible duffel backpack reaches a lower compartment while the top stays closed. Double sliders also let a buyer add a lockable travel feature by sizing the two puller bails to accept a small padlock.
Puller materials
Metal pullers in zinc alloy or stamped steel are the durable default, and they take engraving, debossing or an enamel fill. They add weight and they can clink against the shell, which some brands solve with a small silicone sleeve.
Moulded rubber or PVC pullers are the most common custom option on sports bags. Tooling produces a tab in the brand’s shape and colour, the surface takes a raised logo, and the part is quiet, grippy with wet hands and light. This is the single most cost-effective branding surface on a bag.
Cord pullers with a shrink tip or a moulded end are light, cheap, quick to specify and easy to replace. Reflective cord is a functional upgrade on anything used before dawn, and the cord colour is a free brand cue. The weakness is the attachment: a knotted cord will eventually work loose, and a crimped or heat-sealed termination is what makes the difference.
Fabric and webbing tabs cut from the shell fabric or from 10–15 mm webbing sit flat, cost almost nothing and suit a minimal aesthetic. They wear at the fold over a long life.
Puller choice is where most brands should spend their hardware attention, because it is visible in every product photograph and in every unboxing video. The options and artwork requirements are set out on the custom logo and branding page, and the moulding side sits with custom trims, hardware and accessories.
Bag Buckle Types: Side-Release, Ladder-Lock, Tri-Glide, D-Ring and Cam Buckle
Buckles and adjusters are the second hardware family, and they are specified by width first. The width figure is the webbing width the part accepts, so a “25 mm side-release buckle” takes 25 mm webbing and nothing else.
Part
Common sizes
Material options
Typical load band
Function
Where it belongs
Side-release buckle
20, 25, 38, 50 mm
POM/acetal, nylon, zinc alloy
Light at 20 mm to heavy at 50 mm
Quick-release closure and strap join
Sternum straps at 20 mm, chest and waist straps at 25 mm, compression and haul closures at 38–50 mm
POM (acetal) is the standard for side-release buckles and adjusters. It is dimensionally stable, low friction, resistant to chlorinated water and detergent, and it keeps its spring action across thousands of cycles. It is the right default for a gym, swim or studio bag.
Nylon buckles are cheaper and slightly more flexible, which makes them more forgiving of impact and less consistent under sustained tension. They suit promotional and light-use bags where cost governs, and they are common on corporate and event programmes running at volume.
Zinc alloy buckles and hooks bring weight, a metallic finish and a higher load band. They belong on detachable duffel straps, on cam buckles and on D-rings that carry real load. They also introduce the corrosion questions dealt with below, and they add grams: a set of metal hardware on a 40 L duffel can add 80–150 g against the same set in acetal.
The load bands in the table above are relative descriptors, not rated capacities. A buyer specifying a bag intended to carry heavy equipment should agree a load case with the factory, sample it, and commission a static-load or cyclic test from a laboratory of their choice if the figure needs to appear in retail copy.
Webbing Width for Bag Straps: 20, 25, 38 and 50 mm Compared
Webbing width is the number that ties the whole hardware schedule together, because every buckle, adjuster, hook and ring on the strap must match it. Get the width right and the rest of the strap specification follows.
Polyester webbing is the default on this category. It resists UV, holds printed and sublimated colour well, stretches very little under load so a loaded strap does not sag, and it dries fast after a swim bag or a rained-on commute. Polyester also colour-matches shell fabric more reliably than nylon does, which matters when a brand wants strap and body in one shade.
Nylon webbing is stronger per unit of width and noticeably softer against the neck and shoulder. It also absorbs more water, stretches more under sustained load, and fades faster in sunlight. It earns its place on straps where comfort dominates and where the strap is padded anyway.
Cotton and cotton-blend webbing is a styling choice. It is soft, matte, takes a heritage or minimal look, and it suits everyday sport totes and lifestyle pieces. It is weaker per width, it absorbs water, and it will show sweat and dirt on a shoulder strap faster than polyester.
Thickness, and why it matters more than buyers expect
Two rolls of 38 mm polyester webbing at 1.6 mm and 2.2 mm look identical in a photograph and behave differently on a bag. The thicker roll carries more yarn, resists edge fray longer, and holds a bar-tack better because there is more material for the stitch to bite into. The thinner roll is cheaper, lighter, and softer in the hand, which some brands prefer on a crossbody. Both are legitimate; only one of them is what the buyer thought they ordered. Put the thickness in millimetres next to the width.
Anchoring webbing to the bag
Webbing rarely fails in the middle of its span. It fails where it meets the shell, and that junction is a construction specification rather than a hardware one: the number of bar-tacks, the stitch count, whether a reinforcement patch sits behind the shell fabric, and whether the anchor lands on a seam or on a single panel. On a duffel the strap anchors usually sit on the end panels or across the base, and the way the gusset and base panels are constructed determines how much load reaches the stitching. A strap anchor that lands on a reinforced base wrap is a different component from one that lands on a single layer of 600D, even when the webbing above them is identical.
Zinc Alloy vs Plastic Hardware, Metal Finishes and Custom Moulded Branding
Once the sizes are settled, two decisions remain: what the parts are made of and whether they carry the brand.
Zinc alloy against acetal
Zinc alloy die-casting gives a dense part with a plated finish, sharp detail on an engraved logo and a load band above what moulded plastic offers at the same size. It is also heavier, colder in winter, noisier against a shell, and subject to plating wear. Acetal is lighter, quieter, warmer, chemically stable in chlorinated and salty water, and it cannot be plated, so its colour is whatever it was moulded in.
For sports bags in this category the split is usually functional: acetal for side-release buckles, ladder-locks, tri-glides and cord locks; zinc alloy for D-rings, swivel hooks, cam buckles and zipper pullers where the customer touches the part and reads its weight as quality.
Metal finishes and what wears them
Plated finishes on zinc alloy come in a small standard set: nickel (bright silver), gunmetal (dark grey), matte black, antique brass, and gold. Matte black and gunmetal are usually an electroplated or coated finish over a base plating, which means they carry two layers that can wear at different rates. Bright nickel is the most forgiving in service; matte black is the most likely to show a bright edge where a hook rubs against a D-ring.
Three environments attack plated hardware on this product category:
Chlorine. A swim bag hardware set that sits in a damp pool bag several times a week will show pitting on plated parts within a season. Chloride ions attack the plating at any microscopic pinhole and then work on the zinc base. This is why acetal hardware and coil zippers belong on swim duffel bags, and why a brand that insists on a metal look for a swim range should expect service claims.
Salt. Coastal and beach use produces the same result more slowly. Salt residue left on a hook after a beach day draws moisture and holds it against the plating.
Sweat. The most underestimated of the three. A shoulder strap sits against a damp back and neck for an hour at a time, and human sweat is mildly saline and mildly acidic. Metal hardware positioned at the shoulder-strap adjuster or the sternum clip on a gym backpack sees more corrosion than any other part on the bag.
The design response is simple: keep metal away from skin contact points and away from wet compartments, use acetal at the sternum and strap adjusters, and reserve metal for D-rings, hooks and pullers on the dry face of the bag. Where a buyer wants a metal finish across a range that includes wet products, a salt-exposure or humidity check on the specific plating, commissioned by the buyer from a laboratory of their choice, is the way to find out before the range ships rather than after.
Custom moulded hardware and branded pullers
Standard hardware in a stock colour is the fastest and cheapest route. Custom hardware is what makes a bag look like it belongs to a brand rather than to a catalogue.
Three levels exist. Colour matching takes an existing mould and runs it in a brand colour; there is no tooling, the change is a masterbatch, and the minimum is usually a run quantity rather than a tooling commitment. Logo on an existing part debosses, prints or pad-prints a mark onto a stock buckle or slider; again no tooling, small cost, limited to what the existing surface allows. Custom moulded hardware cuts a new tool for a puller, a buckle face or a strap end in the brand’s own shape.
Custom moulding adds roughly 10–15 days to the development schedule for tooling and first-shot approval, and it carries a one-time tooling cost that is amortised over the parts run from it. The volume at which it makes sense depends on how many units the brand expects to run over the tool’s life rather than on a single order. A brand ordering 300 pieces once will not recover a tool. A private-label programme reordering the same puller across four styles and three seasons usually will, and the tool then belongs to that programme.
The most common first custom part is a moulded rubber zipper puller, because it is visible in every photograph, it is small enough to keep tooling modest, and it works across an entire range without redesigning anything else. The custom trims and hardware page covers what artwork the tooling shop needs, and custom design and structure covers the point at which a hardware change forces a pattern change. Brands weighing the timing should also read the custom graphics and printing options for webbing, since a jacquard or sublimated strap is often a stronger brand signal per unit of cost than a moulded buckle.
How to Write a Hardware Schedule Into a Bag Tech Pack
A hardware schedule is a table in the bill of materials that names every metal and plastic part on the bag, its size, its material, its finish, its brand or acceptable equivalent, how many the bag uses, and where each one sits. Written this way it becomes something the factory quotes against and the inspector checks against.
Here is a worked schedule for a 40 L convertible duffel backpack with a wet compartment and a detachable shoulder strap.
Item
Size
Type
Material
Finish
Brand or equivalent
Qty per bag
Position
Main zipper
#8
Two-way coil, head-to-head, auto-lock sliders
Nylon coil on polyester tape
Colour to match shell, code TBC at lab dip
Nominated brand or approved equivalent, same article across order
1 chain, 2 sliders
Top opening, U-shape, 900 mm chain
Wet-compartment zipper
#5
Reverse-coil, water-resistant film, single non-lock slider
Nylon coil, TPU-faced tape
Black
Same supplier as main zip
1
Base end panel, 400 mm
Front pocket zipper
#5
Coil, single auto-lock slider
Nylon coil on polyester tape
Colour to match shell
Same supplier as main zip
1
Front panel, 300 mm
Interior pocket zipper
#3
Coil, single non-lock slider
Nylon coil on polyester tape
Black
Same supplier as main zip
1
Inside back wall, 200 mm
Zipper puller, main
45 × 12 mm
Custom moulded tab, raised logo
PVC or silicone rubber
Brand colour to Pantone reference
Custom tool, factory-held
2
Both main sliders
Zipper puller, pockets
3 mm cord, 90 mm
Cord loop with heat-sealed tip
Polyester cord, reflective tracer
Black with grey tracer
Stock
3
Pocket sliders
Shoulder-strap webbing
38 mm × 1.8 mm
Woven flat webbing
Polyester
Brand colour, jacquard logo repeat at 150 mm
Nominated mill or equivalent
1.4 m
Detachable shoulder strap
Backpack-strap webbing
25 mm × 1.4 mm
Woven flat webbing
Polyester
Colour to match shell
Stock
1.6 m
Adjustment tails, both straps
Side-release buckle
25 mm
Side-release, dual-adjust
POM/acetal
Black
Stock, one supplier across order
2
Sternum strap and compression
Ladder-lock adjuster
25 mm
Ladder-lock
POM/acetal
Black
Stock
2
Backpack shoulder-strap tails
Tri-glide
38 mm
Tri-glide slide
POM/acetal
Black
Stock
1
Shoulder-strap adjustment
Swivel snap hook
38 mm
Swivel snap hook, spring gate
Zinc alloy
Matte black
Stock
2
Detachable shoulder-strap ends
D-ring
38 mm
Welded D-ring
Zinc alloy
Matte black
Stock
2
End-panel strap anchors, bar-tacked
Cord lock
4 mm
Single-hole spring cord lock
POM/acetal
Black
Stock
1
Internal cinch
Elastic keeper
25 mm
Elastic strap keeper
Nylon elastic
Black
Stock
2
Shoulder-strap tails
The five lines that do the most work
Size in millimetres, not gauge alone. “#5 zipper, chain width 6 mm, tape width 30 mm” cannot be misread. “#5” alone can.
One supplier per family across the order. The clause that stops a bag shipping with three different-looking sliders.
Finish stated as a code or a reference, not a word. “Black” is four different blacks across four suppliers. A Pantone reference or an approved physical sample fixes it.
Quantity per bag. This is what turns the schedule into a costing document and what the factory uses to place hardware orders. A missing quantity means a missed part at cutting.
Position with a dimension. A zipper is only specifiable if its length is stated. A D-ring is only specifiable if its anchor point is drawn on the sketch.
What to ask a supplier about bag hardware
What gauge, chain type and slider lock are you quoting on each opening? Ask for it opening by opening, not as one line.
What is the chain width in millimetres, and the tape width? These separate a real specification from a family label.
Which hardware brand or article number, and will it be the same across the whole order and any reorder? Get the consistency clause in writing.
Are the buckles POM or nylon? They look the same and behave differently after two winters.
What webbing thickness comes with the width you quoted? A 38 mm strap at 1.4 mm is not the strap you costed.
How many bar-tacks at each strap anchor, and is there a reinforcement patch behind the shell? This is where straps actually fail.
Do you check zipper function on finished bags, and on what basis? Ask what the check is, how many bags it covers and what happens to a lot that fails it.
What plating is on the metal parts, and what happens to it around chlorine or sweat? A supplier who has seen the failure will answer in specifics.
What does custom moulded hardware add to the schedule, and at what volume does the tooling make sense for my programme? Expect roughly 10–15 days and a clear amortisation view.
Can I commission a cycle test or a load test on the zipper and strap from a laboratory of my choice? The factory should supply the samples and cooperate with the lab.
Buyers assembling this into a broader sourcing document can fold it into the RFQ checklist, and the structure of the BOM itself, including where the hardware schedule sits relative to fabric and construction, is laid out in the bag tech pack guide. A buyer who wants the hardware section of a quote returned at this level of detail can send the tech pack for a quote or contact the sample room with a hardware question before the rest of the spec is written.
How Venlinker Sources and Checks Bag Hardware
Venlinker is Your Trusted Custom Sports Bag Manufacturer in China, and the hardware schedule is one of the few places where a small specification change reliably shows up in how a finished bag performs two years later. The factory in Huadu District, Guangzhou has run since 2010 across 10+ production lines and 500+ staff, producing 50,000+ bags a month, and hardware is handled as its own material stream rather than as an afterthought to fabric.
Sourcing from the supplier network
Zippers, buckles, webbing, cord and metal trims come through the same material sourcing function that runs the 200+ verified fabric supplier network, with each supplier’s gauges, article numbers, stock colours and lead times held on file. That means a buyer asking for a #8 coil in a specific colour gets an answer about stock and timing rather than a guess. Buyer-nominated hardware is quoted as nominated, alongside an equivalent, so the cost and lead-time consequences of the nomination are visible before the order is placed. Custom moulded pullers and buckles add roughly 10–15 days for tooling and first-shot approval, and that window is quoted up front rather than discovered at production.
Sampling with the real hardware
Samples run in 5–7 working days with one free revision, and they carry the hardware that will go into bulk wherever it is in stock. Where a nominated or custom part will not arrive in time for the first sample, the sample room fits the nearest equivalent and says so on the sample card, so the buyer is never comparing a sample slider against a production slider without knowing it. The sample development page sets out what the sample room needs to hit that window, and a buyer can request a free sample to handle the zipper gauges and webbing widths in person before committing to a schedule.
Incoming inspection and in-line checks
Hardware passes incoming material inspection before it reaches the line. Zipper chain is checked for gauge and chain width, slider fit and lock action; buckles are checked for material, colour against the approved standard and spring return; webbing is measured for width and thickness and checked against the colour reference. During assembly, in-line inspection covers zipper cycle checks on sampled bags, bar-tack counts at every strap anchor and D-ring position, and slider function on loaded bags rather than empty ones. All finished bags go through 100% pre-shipment inspection by the factory’s own team, and third-party inspections from SGS, BV or TUV are welcome on any order, commissioned and paid by the buyer.
MOQ starts at 300 pcs per style per colourway, which lets activewear and fitness brands trial a hardware upgrade on one SKU before rolling it across a range, lets gym and studio chains specify one buckle and webbing standard across duffels, totes and shoe bags, and lets Amazon FBA sellers hold a fixed hardware specification across reorders so listing photographs stay accurate. Factory visits are welcome Monday to Saturday, 40 minutes from Baiyun airport with pickup arranged, and a buyer who wants the hardware line on their quote written properly can ask for a quote with the schedule attached.
Bag Hardware FAQ
What size zipper should I use for a gym duffel bag?
A #8 coil on the main opening, run two-way head-to-head with auto-lock sliders, is the working standard for a 35–55 L duffel. Front and side pockets take #5, an interior valuables pocket takes #3, and a wet or shoe compartment takes #5 in reverse coil. Above 55 L, or on a bag carrying rigid equipment, step the main opening to #10. Below 25 L, a #5 main opening is usually enough, and the weight saving is worth having on a mini gym bag or a light tote.
What is the difference between a #5 and a #8 zipper?
Chain width, mostly. A #5 chain measures roughly 5.5–6.5 mm across when closed and a #8 measures roughly 8–10 mm, with a wider tape and a heavier slider to match. The #8 takes considerably more lateral load before the slider spreads, and it costs and weighs more per metre of chain. The practical decision is load, not size: a #5 is fine on a pocket that holds a phone and keys, and it will fail on a main opening that gets stuffed past its volume every day.
Is a coil or a Vislon zipper better for a sports bag?
Coil, in most cases. Coil is lighter, quieter, more flexible around a curved opening, and it is self-healing, which means a chain forced out of alignment usually reseats when the slider is run back over it. Vislon has a chunkier look, moulds in a brand colour, and carries load well at #8 and #10, but a sheared tooth ends the zipper. Choose Vislon when the zipper is part of the visual identity of the bag and coil for everything else.
Do I have to specify YKK zippers?
No, and buyer-nominated hardware and branded-equivalent hardware are both normal. What matters more than the name on the slider is that the specification is complete (gauge, chain type, chain width, tape width, lock type, finish) and that the same supplier and article number are used across the whole order and any reorder. A nominated brand gives a buyer a stable reference across factories and seasons, at a higher cost tier and sometimes a longer lead time on less common colours and gauges.
What webbing width should a bag strap be?
25 mm for crossbody and waist straps, 38 mm for duffel and backpack shoulder straps, 20 mm for sternum straps and light loops, 50 mm for heavy equipment straps and waist belts. Specify thickness alongside width, typically 1.2–1.6 mm at 25 mm and 1.6–2.2 mm at 38 mm, because two rolls at the same width and different thicknesses cost differently and wear differently. Polyester is the default fibre; nylon is softer and stronger per width but absorbs more water and fades faster.
Should bag hardware be metal or plastic?
Both, in the right places. Acetal for side-release buckles, ladder-locks, tri-glides and cord locks, because it is light, quiet and chemically stable around chlorine, salt and sweat. Zinc alloy for D-rings, swivel hooks, cam buckles and zipper pullers, where weight reads as quality and the load band is higher. Keep metal away from skin contact points and out of wet compartments, since sweat and chlorine attack plating faster than anything else a sports bag meets.
How much does custom moulded hardware add to the timeline and cost?
Tooling and first-shot approval add roughly 10–15 days to development, plus a one-time tooling cost amortised across every part run from that tool. A moulded rubber zipper puller is the usual first custom part, because it is small, visible in every product photograph and reusable across a whole range. Colour-matching an existing buckle or debossing a logo onto a stock part needs no tooling at all and is the faster route for a first order at 300 pcs. The custom trims, hardware and accessories page covers the artwork requirements, and the OEM/ODM workflow shows where tooling sits in the overall schedule.
Summary: Specifying Bag Hardware on Your Next Order
Hardware is the smallest share of a sports bag’s unit cost and the largest share of its warranty risk. A buyer who writes four extra lines into the bill of materials removes most of that risk before the first sample exists.
Specify by gauge and millimetre, opening by opening. A working default for a 35–45 L bag is #8 two-way on the main opening, #5 on pockets and wet compartments, #3 inside, with chain width and tape width stated in millimetres alongside the gauge. Coil is the right chain type for almost everything in this category; Vislon when the zipper is a design feature; metal only on dry, non-contact positions.
Match webbing, buckles and adjusters as one set. Width governs everything: 25 mm for crossbody and waist, 38 mm for shoulder straps, 20 mm for sternum, 50 mm for heavy equipment. State thickness in millimetres, use POM/acetal for buckles and adjusters, zinc alloy for D-rings and hooks, and put the bar-tack count at every anchor into the construction notes.
Fix supplier consistency and finish references in writing. One hardware supplier and article number across the order and every reorder, finishes named by code or approved physical sample rather than by colour word, and custom moulded parts planned with roughly 10–15 days of tooling time in the schedule.
Buyers ready to price a hardware schedule against a real pattern can send the tech pack through the get a quote form, or contact Venlinker to review the hardware section before the rest of the specification is finished. Brands running a first production at 300 pcs will find the volume and timing rules in the custom bag MOQ guide, and distributors and retailers carrying several bag types usually benefit from writing one hardware standard that runs across private label gym bag sets, duffels and backpacks at once.
Need Your Hardware Schedule Quoted Line by Line?
Venlinker builds custom duffels, backpacks, totes and equipment bags for activewear brands, gym and studio chains and Amazon FBA sellers, with zippers, buckles and webbing sourced through a 200+ verified supplier network, buyer-nominated hardware quoted as nominated, samples in 5–7 working days with one free revision, custom moulded pullers in roughly 10–15 days of tooling, zipper and bar-tack checks in line, 100% pre-shipment inspection and MOQ from 300 pcs per style.